The search for a reliable Fully Electric Continuous Pyrolysis Plant is gaining attention as industries seek lower-carbon thermal processing. Electrified reactors can replace direct fossil-fuel burners with controlled heating elements, renewable electricity, and automated temperature management. Picture a steady feed entering the reactor while sensors track heat, pressure, and residence time.
The need is substantial. The World Bank’s What a Waste 2.0 report estimates that global municipal solid waste could reach 3.40 billion tonnes annually by 2050. The Global E-waste Monitor 2024 records 62 million tonnes of electronic waste generated in 2022. These figures show why continuous treatment systems deserve careful evaluation. They do not prove every pyrolysis project will succeed.
Fatih Birol, Executive Director of the International Energy Agency, has stated, “The first fuel of the clean energy transition is energy efficiency.” That principle matters here. A plant’s value depends on more than its electric label. Buyers should examine specific energy consumption, feedstock tolerance, reactor stability, product quality, emissions control, and verified operating history. The IEA’s Energy Technology Perspectives 2024 also emphasizes efficient electrification and clean-energy integration across industrial processes.
This guide compares ten suppliers using publicly available technical information, project evidence, and service capabilities. Claims can be uneven. Some vendors disclose impressive capacity figures but limited long-term data. Others provide strong engineering details without transparent energy results. That gap deserves scrutiny. The strongest candidates should demonstrate safe operation, measurable performance, responsible waste handling, and compliance with applicable environmental standards. A polished brochure is not enough. Real performance is.
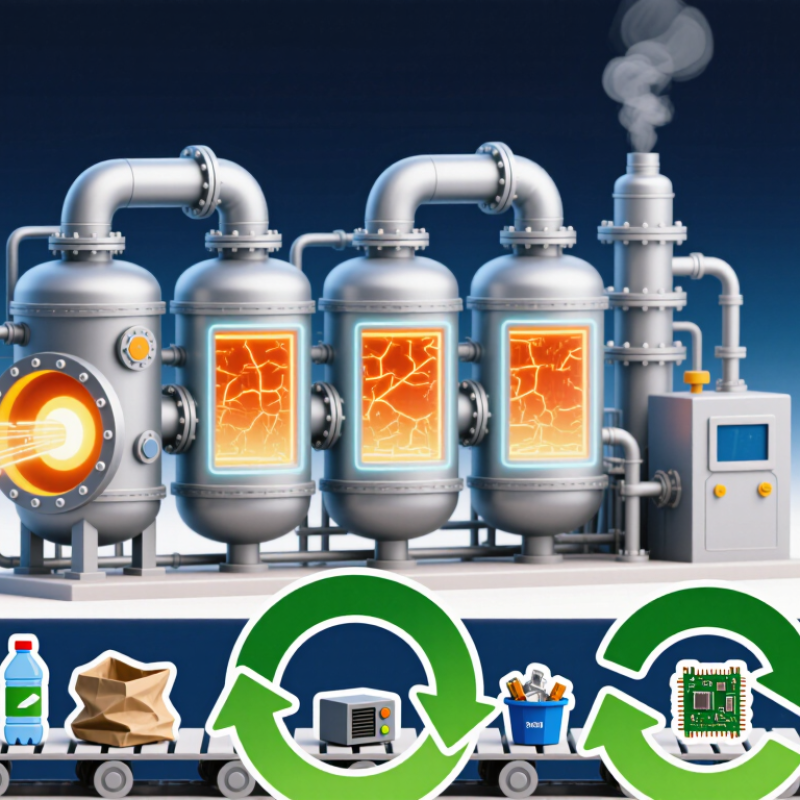
A fully electric continuous pyrolysis plant converts prepared carbon-based feedstock in a sealed, oxygen-limited reactor. Electric heaters supply process heat instead of burning gas or oil directly. The system typically includes feeding, drying, reactor heating, vapor condensation, gas separation, and char discharge. Continuous operation keeps material moving through the reactor, like a slow, controlled conveyor inside a hot steel chamber.
Operating temperatures often range from 400°C to 700°C, depending on feedstock and product targets. Electricity can improve temperature control and reduce direct combustion emissions. However, it is not automatically clean. Its climate performance depends on the electricity mix, heat losses, feedstock preparation, and the final use of pyrolysis oil or gas. The OECD Global Plastics Outlook reported that 353 million tonnes of plastic waste were generated globally in 2019, while only 9% was recycled. This pressure explains growing interest in controlled thermal conversion.
A reliable plant needs moisture control, stable particle size, oxygen monitoring, and continuous condensate management. Small details matter. Wet feedstock wastes energy. Poor sealing creates safety risks and unstable products. The International Energy Agency notes that industrial electrification can reduce emissions when low-carbon electricity replaces fossil heat, but results vary by region. That assumption needs checking. Operators should verify energy consumption per tonne, residence time, emission controls, and independent testing before judging performance. Real data is better than attractive claims.
Fully electric continuous pyrolysis systems convert prepared waste into vapors, gases, and solid char inside an oxygen-limited reactor. Feedstock is shredded, dried, and metered through a sealed screw or rotary feeder. Electric heating elements transfer controlled heat through the reactor wall, avoiding direct combustion inside the chamber.
The process is continuous. Sensors track temperature, pressure, feed rate, and vapor residence time. Hot vapors move to condensers, where liquid fractions separate by boiling range. Non-condensable gas may return to the heating system, reducing external energy demand. Char exits through a cooled discharge unit. Small details matter.
The OECD Global Plastics Outlook reported 353 million tonnes of plastic waste in 2019, while only 9% was recycled. The World Bank’s What a Waste 2.0 estimated global municipal waste could reach 3.4 billion tonnes annually by 2050.
These figures explain the interest in controlled thermal conversion, but they do not guarantee economic success.
Fully electric operation can reduce local combustion emissions and improve temperature precision. Its climate benefit depends on the electricity source, reactor insulation, and actual uptime. The International Energy Agency reported that global electricity generation still produced substantial carbon emissions in 2023, so “electric” does not automatically mean low-carbon.
In field operation, feedstock moisture remains a common weakness. Uneven particles can disturb feeding and create unstable vapor quality. Operators must also inspect seals, condensers, and electrical connections frequently. I would not treat laboratory performance as plant performance. Continuous systems need long-duration data, not attractive short trials.
Selecting a fully electric continuous pyrolysis plant supplier requires more than comparing capacity figures. Start with operating evidence. Ask for documented results from similar feedstocks, including throughput, product quality, energy use, and unplanned downtime. A factory visit can reveal details brochures often hide: uneven heating, dusty control cabinets, or difficult maintenance access.
Review the heating system carefully. Electric elements should provide stable temperatures across the reactor, not only near sensors. Request thermal mapping, control logic, insulation data, and a clear energy balance. The supplier should explain how the system responds to changing moisture levels and feedstock size. Small variations matter. They affect yield, power demand, and product consistency.
Safety and compliance deserve equal attention. Check emergency shutdowns, ventilation, fire protection, electrical certifications, and emissions monitoring. Reliable suppliers provide drawings, risk assessments, operating manuals, training, spare-parts plans, and responsive technical support. Speak with previous customers, but test their claims against maintenance records and production data. A polished reference is not enough. Some evaluations also overlook local installation skills and grid capacity. That can become an expensive surprise. I would score suppliers using total ownership cost, not purchase price alone. Include electricity consumption, labor, cleaning time, replacement parts, commissioning support, and future upgrades. No supplier gets every answer right. The most credible one explains limitations clearly and shows how its design manages them.
This chart presents a practical screening framework for comparing fully electric continuous pyrolysis plant suppliers. The percentages represent suggested evaluation weights rather than the performance of any specific company. Priority is given to energy efficiency, stable continuous operation, temperature control, emissions management, and long-term maintainability.
The top ten fully electric continuous pyrolysis plant suppliers should be judged by engineering evidence, not brochure claims. World Bank research estimates global municipal waste will reach 3.88 billion tonnes annually by 2050. This growing pressure increases demand for stable, lower-emission thermal processing systems. However, fully electric heating does not automatically mean zero emissions. The electricity source, feedstock preparation, and gas treatment still matter.
Reliable suppliers should disclose reactor temperature uniformity, throughput testing, electricity consumption, and product quality data. A practical reference point is continuous operation above 90% availability, although site conditions can reduce this figure. The Global E-waste Monitor 2024 reports 62 million tonnes of electronic waste in 2022, showing how quickly difficult feedstocks are growing. Suppliers must explain whether their equipment handles tires, plastics, biomass, or mixed materials. They are not interchangeable.
Look closely at maintenance access. Operators need visible temperature sensors, automatic feeding, emergency shutdowns, and documented inspection schedules. Third-party testing strengthens credibility. ISO-based quality procedures also help, but certification alone proves little about real production. I would request a monitored trial using representative feedstock. Small gaps appear there. Energy figures often exclude shredding, cooling, and gas cleaning, which can distort comparisons. Suppliers must state those boundaries clearly. That is more convincing than an impressive headline.
Choosing among the top 10 fully electric continuous pyrolysis plant suppliers requires more than comparing prices. Your feedstock should guide the decision. Moisture, particle size, contamination, and daily volume affect reactor performance. Ask each supplier for test results using material similar to yours.
Look closely at the heating system. Fully electric operation can reduce direct fuel use, but electricity demand may be substantial. Request measured energy consumption, temperature stability records, and expected production capacity. A reliable supplier should explain maintenance access, spare-part availability, operator training, and emergency procedures. Ask for references from operating facilities, not only photographs. Site visits can reveal noise, dust control, housekeeping, and actual workflow. No checklist is perfect. Your assumptions may still need testing.
Tips: Prepare a written specification before contacting suppliers. Include feedstock analysis, target output, operating hours, local power limits, and site conditions. Request a pilot trial or sample evaluation when possible. Check whether the proposed system meets local environmental, electrical, fire, and waste-handling requirements. Compare warranty terms carefully, especially for heating elements, controls, and continuous feeding equipment. A low quotation can hide installation costs, software limitations, or long delivery times. Ask who responds when production stops at midnight.
| Rank | Anonymous Supplier Profile | Typical Plant Capacity | Suitable Feedstock | Heating Configuration | Typical Operating Temperature | Continuous-Feed Features | Key Selection Strength | Important Verification Point |
|---|---|---|---|---|---|---|---|---|
| 1 | Supplier Profile 01 | 5–20 tonnes per day | Waste tires, rubber products, selected plastics | Electric resistance heating with insulated reactor chambers | 400–550°C, feedstock dependent | Sealed feeding, automatic temperature control, non-condensable-gas recycling | Strong fit for tire-to-oil and recovered carbon projects | Confirm product specifications, gas-cleaning design, and electrical load at rated capacity |
| 2 | Supplier Profile 02 | 10–30 tonnes per day | Mixed plastic waste, PE, PP, and PS | Electric heating zones with independent PID control | 380–520°C | Metered screw feeder, vapor cyclone, staged condensation | Suitable for modular plastic-waste recycling lines | Check tolerance for PVC, moisture, fines, and non-plastic contaminants |
| 3 | Supplier Profile 03 | 20–50 tonnes per day | Biomass residues, agricultural waste, wood by-products | Electric externally heated rotary reactor | 350–600°C | Automatic solids discharge, moisture monitoring, char cooling | Good option for biochar and soil-amendment applications | Validate feedstock preparation, residence time, and biochar quality data |
| 4 | Supplier Profile 04 | 3–12 tonnes per day | Sawdust, rice husks, shells, and other dry biomass | Electric batch-preheat and continuous reactor heating | 350–500°C | Compact footprint, automatic feeding, cyclone dust separation | Appropriate for decentralized and small industrial projects | Confirm continuous operation under the actual moisture content of the feedstock |
| 5 | Supplier Profile 05 | 15–40 tonnes per day | End-of-life tires and rubber waste | Multi-zone electric heating with thermal insulation | 420–550°C | Continuous wire separation, oil condensation, char discharge | Focused configuration for tire recycling and material recovery | Review steel-wire handling, char purity, emissions control, and operating labor |
| 6 | Supplier Profile 06 | 8–25 tonnes per day | Agricultural residues and low-ash biomass | Electric induction-assisted reactor heating | 400–650°C | Variable-speed feeder, oxygen-limited operation, gas recirculation | Fast thermal response for changing biomass feed rates | Verify reactor material compatibility, induction efficiency, and maintenance requirements |
| 7 | Supplier Profile 07 | 25–60 tonnes per day | Pre-processed plastic film, packaging waste, and polyolefins | Electric heating with multiple independent temperature zones | 400–530°C | High-throughput screw reactor, feed de-airing, automated condensate collection | Designed for larger commercial plastic-recovery facilities | Request demonstrated throughput using feedstock with comparable contamination levels |
| 8 | Supplier Profile 08 | 5–18 tonnes per day | Sewage sludge, digestate, and dried organic solids | Electric indirect heating with sealed solids handling | 450–650°C | Feed drying integration, enclosed conveyors, dust and odor control | Potential fit for controlled organic-waste treatment | Check regulatory requirements, contaminant concentration, and char disposal conditions |
| 9 | Supplier Profile 09 | 10–35 tonnes per day | Mixed rubber, plastics, and selected industrial residues | Electric heating with heat recovery from process gas | 400–600°C | Automated feed metering, gas scrubber, oil-water separation | Flexible configuration for multi-feedstock projects | Insist on feedstock-specific trials because mixed inputs can change oil yield and gas composition |
| 10 | Supplier Profile 10 | 2–10 tonnes per day | Small-volume plastic, rubber, and biomass waste streams | Fully electric modular reactor with plug-in auxiliaries | 350–550°C | Skid-mounted modules, PLC control, compact condensation system | Lower initial scale and easier phased expansion | Evaluate cost per tonne, spare-parts availability, commissioning support, and expansion limits |
How to Select the Right Supplier
Compare suppliers using feedstock testing, guaranteed throughput, electricity consumption, product yield, emission-control performance, automation level, installation requirements, warranty coverage, after-sales service, and total cost of ownership. Capacity and temperature figures are indicative engineering ranges; final values should be confirmed through a feedstock-specific trial, process guarantee, and detailed technical proposal.